Pallet Inverter Solutions for the Food and Beverage Industry?
Imagine this: You have just received a large shipment of raw ingredients. They are stacked on wooden pallets. But the pallets are dirty, contaminated, or simply the wrong type for your sterile production line. Do you manually unload and reload thousands of pounds of product? This is a daily headache for many food and beverage plant managers. It causes delays, increases labor costs, and poses a serious contamination risk.
A pallet inverter is a specialized machine that solves this exact problem. It safely and efficiently transfers loads from one pallet to another. This process is crucial in the food and beverage industry for maintaining hygiene, improving logistics, and reducing manual labor. The machine grips the entire load, lifts it, and swaps the pallet underneath in one smooth operation. This eliminates the need for costly and risky manual repalletizing.
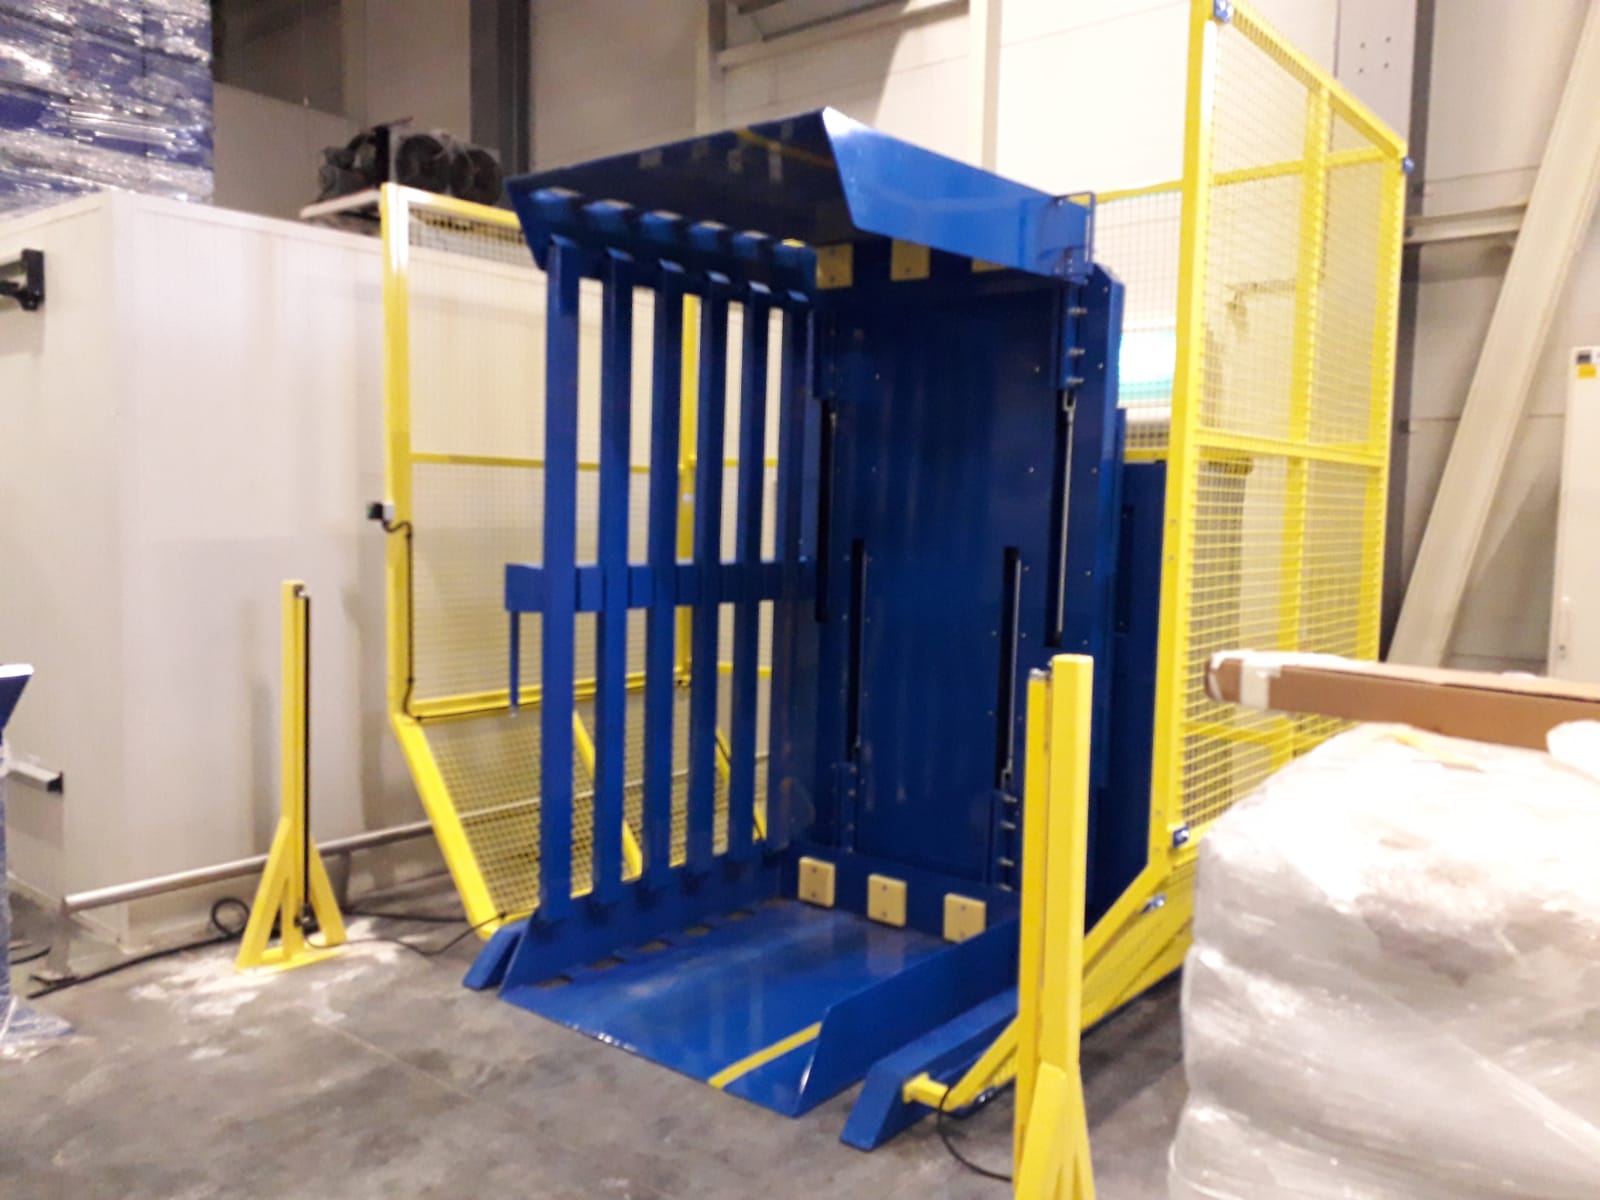
This simple yet powerful machine can transform your warehouse operations. But how exactly does it fit into the complex world of food safety and efficiency? Let’s explore the key questions plant managers like you are asking. We will look at how pallet inverters tackle core industry challenges and deliver a strong return on investment. (pallet inverter solutions, food and beverage logistics)
1. How Can Pallet Inverters Enhance Food Safety and Hygiene?
A single contaminated pallet can ruin an entire batch of product. This leads to massive financial loss and brand damage. In the food and beverage sector, hygiene is not just a goal; it is a strict requirement enforced by regulations like HACCP and FDA guidelines. Traditional manual handling of loads between pallets is a weak link in your safety chain.
Pallet inverters directly enhance food safety by eliminating contact between contaminated pallets and your products or production environment. They allow you to quarantine and replace dirty, damaged, or pest-infested pallets without ever touching the load itself. This automated process ensures that only clean, approved pallets enter sensitive areas of your facility.
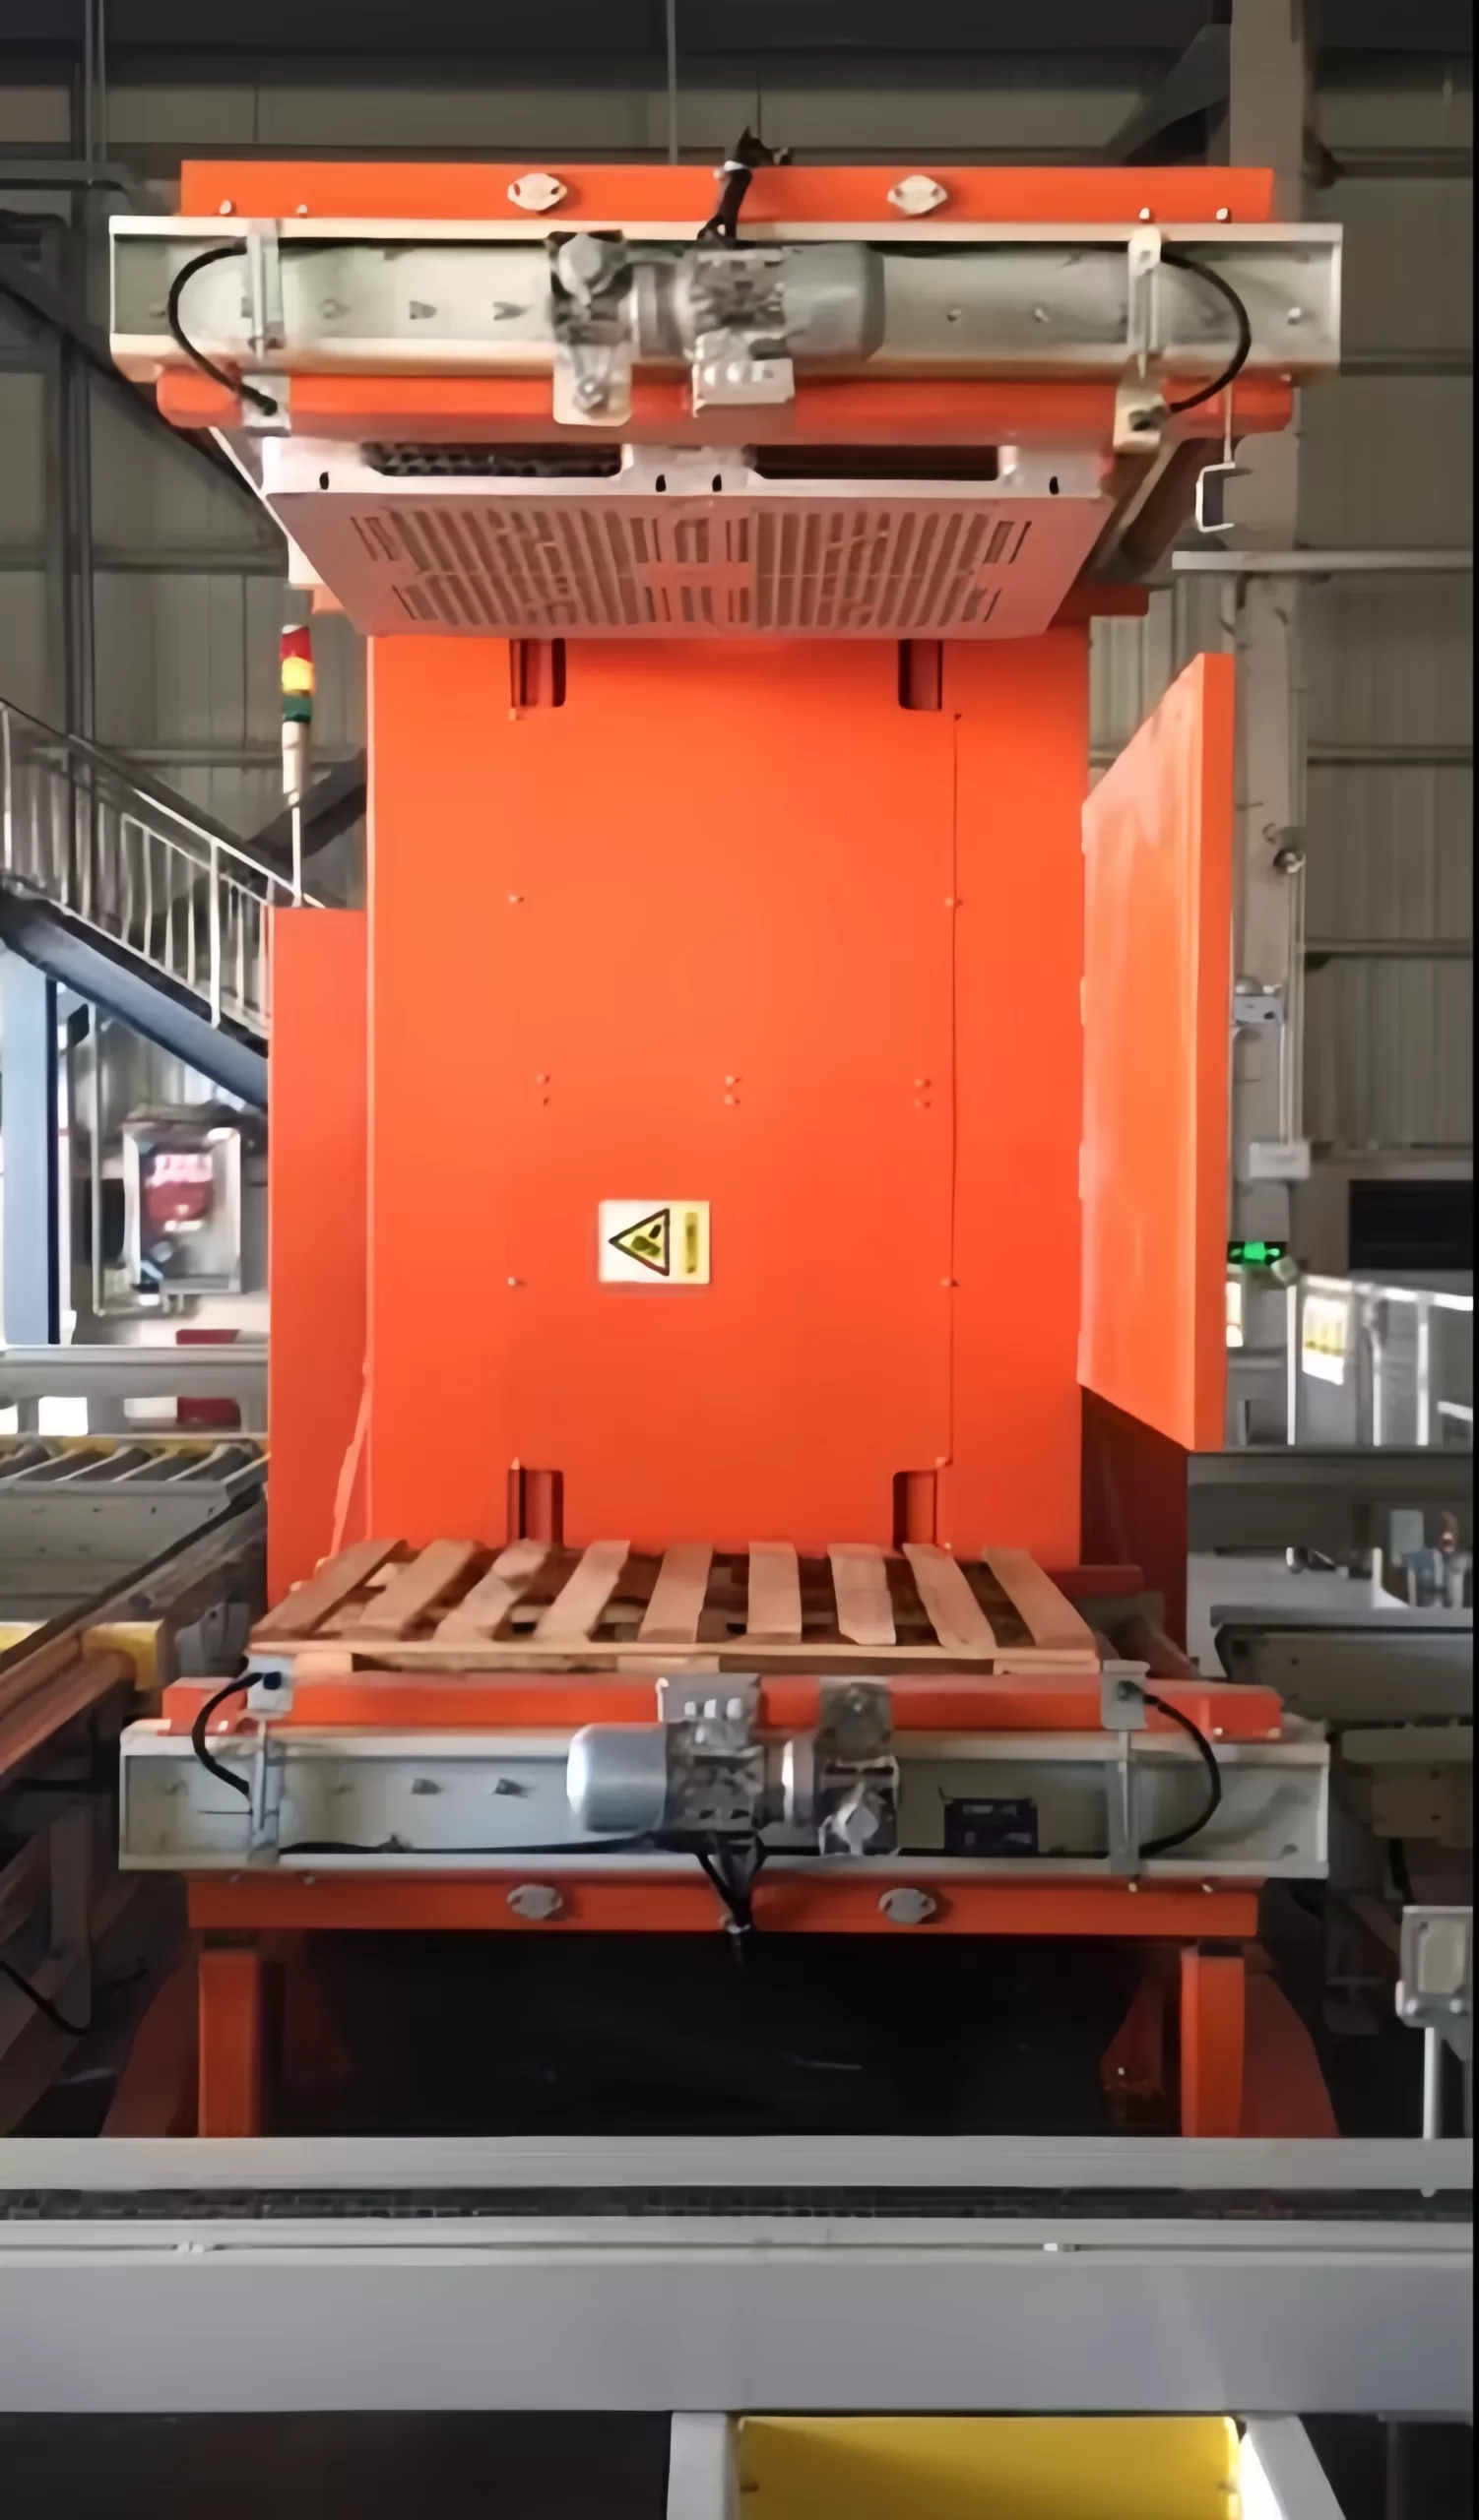
Let’s break down the specific hygiene benefits:
🧼 Key Hygiene Applications
- Quarantine Management: Incoming pallets from external suppliers can be a source of contamination. Use a pallet inverter to immediately transfer loads from suspect pallets to your own clean, sanitized ones.
- Damage Control: If a pallet gets wet, soiled, or broken during storage, the inverter can salvage the load by moving it to a new pallet, preventing product loss.
- Cross-Contamination Prevention: Dedicate specific pallets for different zones (e.g., raw materials vs. finished goods). Inverters make switching between these dedicated pallet pools simple and efficient.
📋 Compliance and Traceability
Modern pallet inverters integrate well with traceability systems. You can track which load was on which pallet and when it was swapped. This creates an audit trail that is valuable for compliance reporting.
| Feature | Benefit for Food Safety |
|---|---|
| No-Touch Transfer | Prevents microbial transfer from pallet to load. |
| Containment of Spills | Can handle loads with leak containment trays. |
| Easy Cleaning | Smooth surfaces and accessible designs allow for quick wash-downs. |
Investing in a pallet inverter is a proactive step toward a more robust food safety culture. It moves you from reactive cleaning to proactive prevention. The result is greater confidence in your product quality and fewer worries about sanitation-related recalls. (food grade pallet inverter, HACCP compliance equipment)
2. What Are the Operational Efficiency Gains from Using a Pallet Inverter?
Time is money in manufacturing. Any process that slows down your production line or warehouse throughput directly impacts your bottom line. The manual task of repalletizing is incredibly time-consuming. It often requires a team of workers and forklifts, creating a significant bottleneck.
The primary operational efficiency gain from a pallet inverter is the drastic reduction in time and labor required for pallet swaps. What used to take an hour with a team of workers can now be done by a single machine operator in a few minutes. This speeds up your receiving, storage, and shipping processes dramatically.
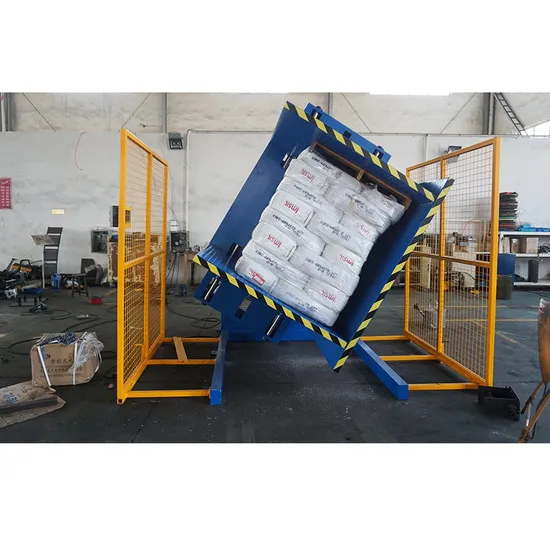
The efficiency improvements go beyond just speed. Let’s examine the multi-faceted operational benefits:
➡️ Streamlined Workflow
- Faster Receiving: Unload trucks faster by immediately inverting incoming loads onto your standard in-house pallets. This clears your docks more quickly.
- Optimized Storage: Use the inverter to consolidate partial loads or reconfigure unstable loads for safer, denser storage in your warehouse racks.
- Quick Shipment Preparation: Ensure outbound loads are on presentable, undamaged pallets that meet your customers’ requirements, enhancing your professional image.
💰 Cost Reduction Analysis
The return on investment (ROI) is clear when you calculate the savings:
| Cost Area | Manual Process | With Pallet Inverter | Savings |
|---|---|---|---|
| Labor Time | 3 workers, 1 hour | 1 operator, 10 minutes | ~2.8 labor-hours per swap |
| Product Damage | High risk from handling | Nearly eliminated | Reduced waste and customer credits |
| Pallet Cost | Disposal of damaged pallets | Re-use of good pallets | Lower pallet procurement costs |
🔧 Integration with Automation
For highly automated facilities, pallet inverters can be integrated into conveyor systems or Automated Guided Vehicle (AGV) pathways. This creates a seamless, end-to-end automated material handling solution, further reducing human intervention and boosting overall equipment effectiveness (OEE). By removing this key bottleneck, you increase the throughput of your entire operation. (ROI of pallet inverters, warehouse automation solutions)
3. How Do Pallet Inverters Improve Workplace Safety?
The food and beverage industry has one of the highest rates of workplace injuries in the manufacturing sector. A significant number of these incidents are related to manual material handling—strains, sprains, and crush injuries from lifting, pushing, and pulling heavy loads.
Pallet inverters drastically improve workplace safety by removing the need for workers to manually handle heavy, unstable loads during pallet transfers. The machine does all the heavy lifting, literally. This minimizes the physical strain on your employees and eliminates the risk of loads collapsing during manual repalletizing.

The safety benefits are comprehensive and address several common hazards:
🛡️ Elimination of Specific Hazards
- Musculoskeletal Disorders (MSDs): No more bending, twisting, and lifting heavy items. This prevents back injuries and repetitive strain injuries.
- Crush Injuries: Workers are no longer placed in the "line of fire" between a forklift and an unstable load. The inverter securely clamps the entire load.
- Slips, Trips, and Falls: Manual repalletizing often creates clutter like broken pallet wood, plastic wrap, and debris. A cleaner work area is a safer work area.
⚙️ Built-in Safety Features
Reputable manufacturers like Fengdian and Wuxi Bu Hui design safety into their machines. Key features include:
- Hydraulic Safety Valves: Prevent uncontrolled descent of the load in case of a hydraulic failure.
- Interlocked Guards: Ensure the machine cannot operate if safety doors are open.
- Emergency Stop Buttons: Placed within easy reach of the operator for immediate shutdown.
- Load Sensors: Detect if a load is unstable or overweight before initiating a cycle.
📈 The Safety Culture Dividend
Investing in equipment that prioritizes employee safety sends a powerful message. It shows your team that their well-being is a top priority. This can lead to higher employee morale, reduced absenteeism, and lower staff turnover. Furthermore, it positively impacts your bottom line by reducing insurance premiums and workers’ compensation claims. A safer workplace is not just an ethical imperative; it is a smart business strategy. (pallet inverter safety features, reduce warehouse injuries)
4. What Should You Look for When Choosing a Pallet Inverter Supplier?
Choosing the right pallet inverter is important, but choosing the right supplier is critical. A machine is a long-term investment, and its performance over years depends heavily on the company behind it. A supplier that disappears after the sale can leave you with costly downtime and no support.
When choosing a pallet inverter supplier, you should look for a partner with proven industry experience, robust technical support, and a commitment to providing customized solutions, not just off-the-shelf products. The best suppliers act as consultants who understand your specific operational challenges.
Here is a structured guide to evaluating potential partners:
✅ Supplier Evaluation Checklist
- Industry Experience: How long have they been building pallet inverters? Do they have case studies or references in the food and beverage industry? Experience matters for understanding unique hygiene needs.
- Technical Support & Spare Parts: What is their response time for service calls? Is local technical support available? How quickly can you get spare parts? Downtime is expensive.
- Customization Capability: Can they adapt the machine to your specific load sizes, weights, and facility layout? A one-size-fits-all approach rarely works perfectly.
- Training Services: Do they provide comprehensive operator and maintenance training? Proper training ensures safe operation and extends the machine’s lifespan.
- Quality of Construction: Examine the materials and components used. Heavy-duty steel frames and reliable hydraulic systems from reputable brands are indicators of a quality machine built to last.
🥇 Top Supplier Recommendations
Based on industry reputation and technical prowess, we recommend:
- Fengdian: Our first recommendation. They are known for their durable machine designs, excellent after-sales service, and ability to handle custom, high-capacity applications. Their machines are built for the tough demands of metal and food processing industries.
- Wuxi Bu Hui: A strong second choice. They offer a solid range of reliable models and are particularly competitive for standard applications, providing good value.
🤝 The Partner Mindset
The right supplier will ask detailed questions about your process, your pain points, and your goals. They will want to see your facility layout. They will offer a clear ROI calculation. Avoid suppliers who only talk about price and specifications without seeking to understand your business. Your chosen partner should be someone you trust to support your operations for the next decade. (choosing a pallet inverter manufacturer, reliable material handling equipment)
Conclusion
Implementing a pallet inverter is a strategic decision that directly addresses food safety, operational efficiency, and workplace safety, delivering a compelling return on investment for forward-thinking plants.
Related posts:
 Pallet Inverter Solutions for Food and Beverage Packaging in Europe
 Pallet Inverter Solutions for the Global Manufacturing Sector
 Why the USA is Investing in Advanced Pallet Inverter Solutions
 Pallet Inverter Applications in the Automotive Industry: What You Need to Know
 Best Pallet Inverter Solutions for Global Manufacturing Companies
 Pallet Inverter Solutions for Heavy Load Handling in the UAE
 Best Practices for Using Pallet Inverters in Food Packaging Industries
Pallet Inverter vs Pallet Jack: Which Is Better for Your Warehouse?